From Requirements to Sign Off: A Practical High Speed Channel Checklist
Most problems found at sign-off were decided much earlier: a laminate picked by habit, a budget never written down, a fast pair routed next to a split plane. A short checklist, worked in order, catches them while they are still cheap to fix.
Why order matters
Each decision constrains the next. The interface sets the loss budget. The budget and route length set the laminate. The laminate sets trace width for a target impedance. Traces and groups shape the stackup, and the stackup shapes the vias and ball map.
Work out of order and you rework. That is why FlowSimLab's dashboard lays the setup out as numbered steps, each one feeding the next.
The checklist
1. Requirements and material
- Fastest data rate and signalling written down, Nyquist calculated.
- Longest route and its loss budget known.
- Layer count, lead-free assembly and environment agreed.
- Laminate chosen for loss at Nyquist, thermal limits and cost.
- Datasheet Er and Df flagged for confirmation with the fab.
More on this in The Role of Data Rate in Laminates Thermal Limits and Cost Tradeoffs.
2. Channel budget
- Every part listed from transmitter to receiver.
- Interface budget and margin entered, not assumed.
- Total loss inside budget, with the headroom recorded.
- Maximum PCB length known before layout starts.
3. Trace impedance
- Microstrip or stripline chosen for each route.
- Width solved for the target on the real stackup and copper.
- Tolerance agreed, typically ±10%, and met.
- Delay and loss per inch recorded.
The budget and impedance steps are worked through in How to Budget Loss and Impedance for Multi Layer PCB Stacks.
4. Net groups
- Nets grouped by interface, with shared rules.
- Skew tolerance, spacing and maximum via count set.
- Crosstalk risk checked for each group.
5. Stackup
- Every fast layer next to a solid reference plane.
- Board thickness within tolerance of the target.
- Stackup symmetric to avoid warp.
- Groups assigned to layers, with via stubs in mind.
6. Package and ball map
- Signal-to-ground ratio chosen for the fastest interfaces.
- Every high-speed ball has a neighbouring return.
- Path from each bump to its layer checked for stub length.
See Chip Packaging Transitions from Package to Board Explained.
7. Standards and sign-off
- Each channel checked against its interface standard.
- Every "check" or "fail" either fixed or explained in writing.
- First-article measurements correlated with the model.
Let the last step summarise the others
Sign-off should not be a fresh analysis. It should read back the decisions already made.
FlowSimLab's Standards step does exactly that: it pulls the material, channels, trace types and stackup from the earlier steps and checks each channel against its interface.
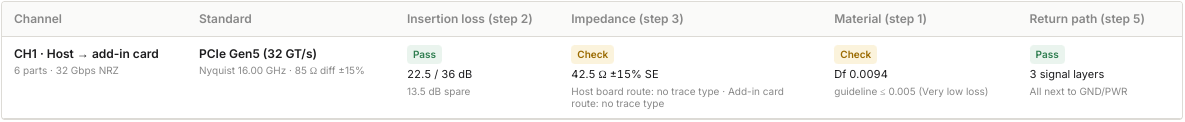
A flag is useful. Here, the routes have not yet been linked to a trace type, so impedance cannot be confirmed, and the laminate sits above the Gen5 guideline. That is exactly the kind of gap a checklist exists to catch. How each check works is explained in How to Use Standards Checks to Accelerate PCB Sign Off.
Use it every time
Print the checklist, or simply work through the dashboard in order. A channel that reaches sign-off with every box ticked has very few surprises left. For the full walkthrough, read Step by Step Channel Setup Using FlowSimLab DSS for High Speed Designs.